

In the global trade and deep-processing supply chain of cashew kernels, precision grading is not merely a baseline for food safety, but a critical determinant of commercial value and the key to meeting diverse application scenarios. However, traditional sorting methods exhibit significant limitations in actual production: physical sieves can only perform rough grading based on particle size, failing to identify differences in appearance quality; manual sorting is not only inefficient but highly susceptible to worker fatigue and subjective judgment discrepancies, leading to quality inspection standard drift; intelligent belt-type vision-based sorting systems primarily focus on removing defective products and foreign material to ensure food safety and basic appearance, with their sorting logic largely confined to a binary "pass/fail" judgment, lacking the capability for multi-dimensional, precision grading of cashew kernels.
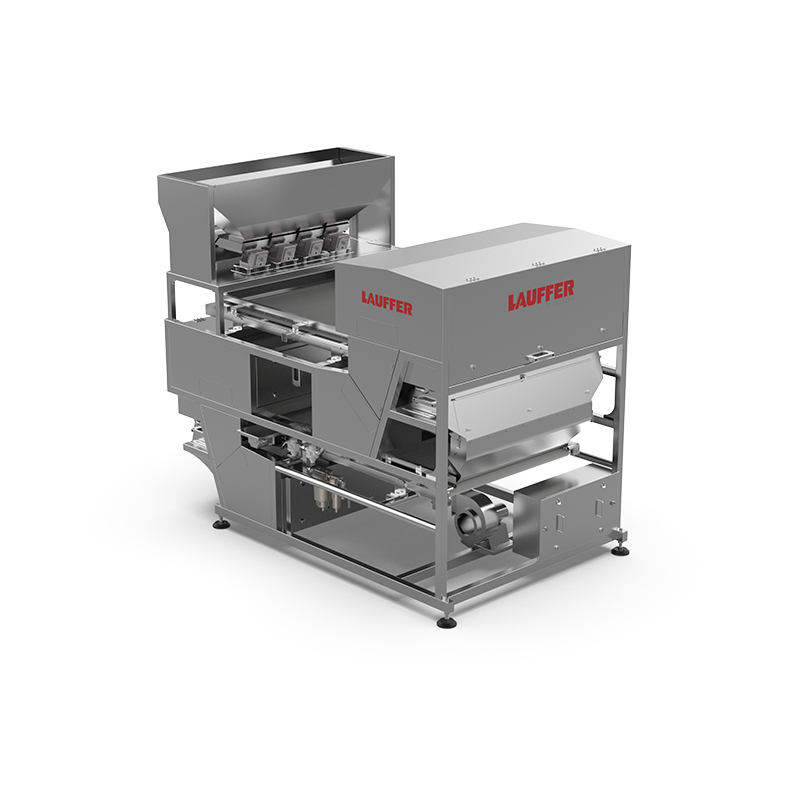
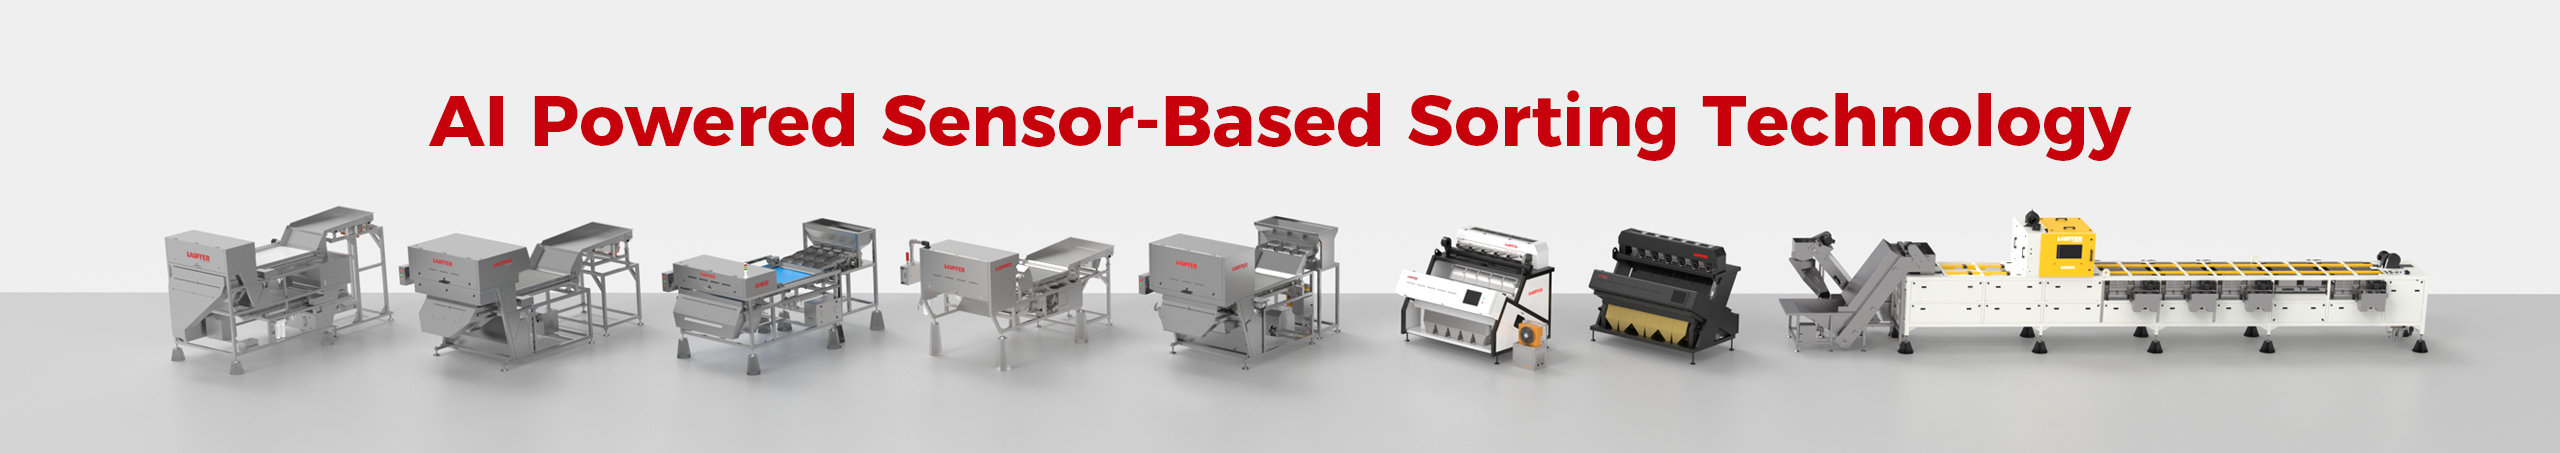
The Demeter C Series is an intelligent vision-based grading system tailored for this exact scenario. Featuring 360° inspection and a multi-array (4 or 8 groups) roller-type sorting structure, the system deeply integrates hyperspectral imaging (HSI) and high-resolution RGB (HR-RGB) VIS imaging technologies. Leveraging proprietary AI deep learning algorithms for real-time scanning and surface feature analysis on cashew kernels, and paired with high-performance air ejectors, it achieves precision classification into up to 16 grades in a single pass, strictly adhering to international trade standards for cashew kernels. This significantly enhances sorting efficiency while maintaining exceptional grading accuracy.
Empowered by AI-driven surface feature recognition, the system continuously learns from real production data, steadily improving its detection accuracy. This means the equipment's performance is not static after deployment; instead, it continuously adapts and improves as production data accumulates, delivering stable and reliable sorting performance. This enables cashew kernel processors consistently deliver high-quality products that meet stringent international standards, securing a competitive edge in the fiercely competitive global market.
Technical Features
● Tailored Vision-Based Grading System for Premium Cashew Kernels
✦ High-Performance Uniform Feeding
Ensures cashew kernels enter the inspection zone evenly and stably, minimizing inspection interference, and providing consistent input conditions for subsequent high-precision grading.
✦ Customized Anti-Breakage Roller Structure
Accommodates the curved and fragile nature of cashew kernels through an exclusive roller-type conveying system, ensuring stable high-throughput transport while minimizing mechanical impact and kernel breakage to balance processing efficiency with product integrity.
✦ 360° Dead-Zone-Free Inspection
Executes individual, all-around scanning and analysis on every single cashew kernel, enabling efficient grading based on preset standards, and significantly reducing missed detections or misjudgments caused by posture occlusion.
● AI Powered Ultra-High-Precision Defect Inspection System
✦ Area-Scan High-Resolution RGB (HR-RGB) VIS Imaging
Captures surface features of materials from 360° in all directions, providing reliable image input for AI algorithms to achieve precision grading across multiple dimensions.
✦ Proprietary AI Deep Learning Algorithms
Enhances surface feature recognition and supports model retraining with real-world production data, continuously improving the detection accuracy through deep learning.
✦ Ring-Shaped Shadowless Illumination
Provides uniform, shadow-free lighting, helping to maintain consistent imaging quality, and ensuring the reliability of visual recognition.
Based on surface features, the system achieves ultra-high-precision, multi-dimensional, and precision grading in strict accordance with international trade standards for cashew kernels:
Simultaneous Defect & Size Sorting
✩ Color Defects: Black spots, oxidation, yellowing
✩ Shape Defects: Broken, cracked, shriveled, deformed
✩ Processing Defects: Shell residues, adhered testa even minor testa
✩ Biological Contaminants: Insect damage, mold, rotten
✩ Size Grading: Whole (W), SW(Super Whole), S(Splits), B(Butts)

✦ Adapts to global cashew types (Vietnam, India, Africa)
● In-House High-Performance Air Ejector System
✦ Optimized Ejector Valve Design
Balances durability, response speed, and air consumption efficiency, maintaining stable performance even under long-term, high-frequency operation.
✦ High-Speed, High-Precision Ejection
Delivers millisecond-level response and precise material rejection, ensuring optimal sorting accuracy even under high-throughput conditions.
✦ Reduced Operating Costs
Significantly lowers the false reject rate, minimizing material waste from good products being incorrectly ejected, while optimizing air consumption to reduce overall operational expenses.
● 15-Inch Industrial Touchscreen Control System
✦ Intuitive Interaction
User-friendly human-machine interface (HMI) with multi-language support.
✦ One-Click Switching
Quickly recalls sorting parameters for different products.
✦ Comprehensive Remote Support
✩ Remote access and real-time monitoring
✩ Performance data dashboard
✩ Online expert diagnostics
✩ Interactive troubleshooting